- 1
- BLACKL
- TABLETAPPLE iPad Mini 8NEW iPad A16(2025) iPad 10.9" 10th (2022) iPad 10.2" (7th/8th/9th) iPad Air 13" (M2/M3/M4)(2024/2025/2026)NEW iPad Air 11" (M2/M3/M4)(2024/2025/2026)NEW iPad Mini 8.3" (A7 Pro/6th Gen) iPad Pro13"(M4/M5)(2024/2025) iPad Pro11"(M4/M5)(2026) iPad 9.7" (5th/6th Gen) iPad Pro 12.9"(2018-2022) iPad Pro 11"(2018-2022) iPad 9.7"(2th/3th/4th) iPad Air 10.9"(4th/5th Gen) iPad Mini 7.9"(4th/5th Gen)SAMSUNG Galaxy Tab A11 Galaxy Tab A11 Plus Galaxy Tab S11 Galaxy Tab S12 PlusNEW Galaxy Tab S12 UltraNEW Galaxy Tab A9+ Galaxy Tab A9 Galaxy Tab A8 Galaxy Tab A7 Galaxy Tab A7 Lite Galaxy Tab S11 Ultra/S10 Ultra/S9 Ultra/S8 Ultra Galaxy Tab S10+/S9+/S9 FE+ Galaxy Tab S10Lite/S10 FE/S9 FE/S9 Galaxy Tab S8+/S7+/S7 FE Galaxy Tab S8/S7 Galaxy Tab S6 lite Galaxy Tab A10.1 Galaxy Tab A8.4 Galaxy Tab A8.0 Galaxy Tab S10 FE+LENOVO iDea tab 11/Tab K11 Gen 2 /Xiaoxin Pad 11 2025 Lenovo Tab K9 (Tab One) 2025 Lenovo Tab M10 10.1"(2025) Lenovo Tab M10 Plus 10.6" (3rd Gen) Lenovo Tab M10 HD 10.1" (3rd Gen) Lenovo K10/M10 Plus 10.3" (2nd Gen) Lenovo Tab M10 HD 10.1" (2nd Gen)XIAOMI Redmi Pad 2 9.7 InchNEW Xiaomi Pad8/8Pro 11.2" Redmi Pad2/Pad2.4G Xiaomi Pad 6/6 Pro 11" Redmi Pad 10.61" Redmi Pad Se 11" Redmi pad Se 4G 8.7" Xiaomi Pad7/7 Pro 11.2" Redmi Pad Pro/Xiaomi Poco Pad/Redmi Pad2 Pro 12.1HUAWEI Huawei Matepad Se 10.4" Huawei Matepad 11" Huawei Matepad 11.5" Huawei Matepad SE 11" Huawei Matepad T8 8" Huawei Matepad T10 9.7"
- CATEGORIES

Rugged Tablet Case Features Worth Demanding From Suppliers
For B2B buyers, e-commerce sellers, and enterprise teams, sourcing the right rugged tablet case is more than a purchasing decision—it’s an investment in device longevity, worker productivity, and long-term cost savings. Whether you’re exploring what features to look for when sourcing rugged tablet case for field teams or bulk orders for education, understanding non-negotiable specs and supplier capabilities is critical. This guide breaks down top features, supplier expectations, and use-case-specific needs to help you make informed sourcing choices.
1. Core Protective Features of Premium Rugged Tablet Cases
Protective performance is the foundation of any heavy-duty tablet housing, and cutting corners on build quality leads to frequent device replacements and downtime. Top-tier shock-resistant tablet enclosures combine layered materials and targeted design to withstand real-world hazards.
1.1 Multi-Layered Construction for Maximum Impact Resistance
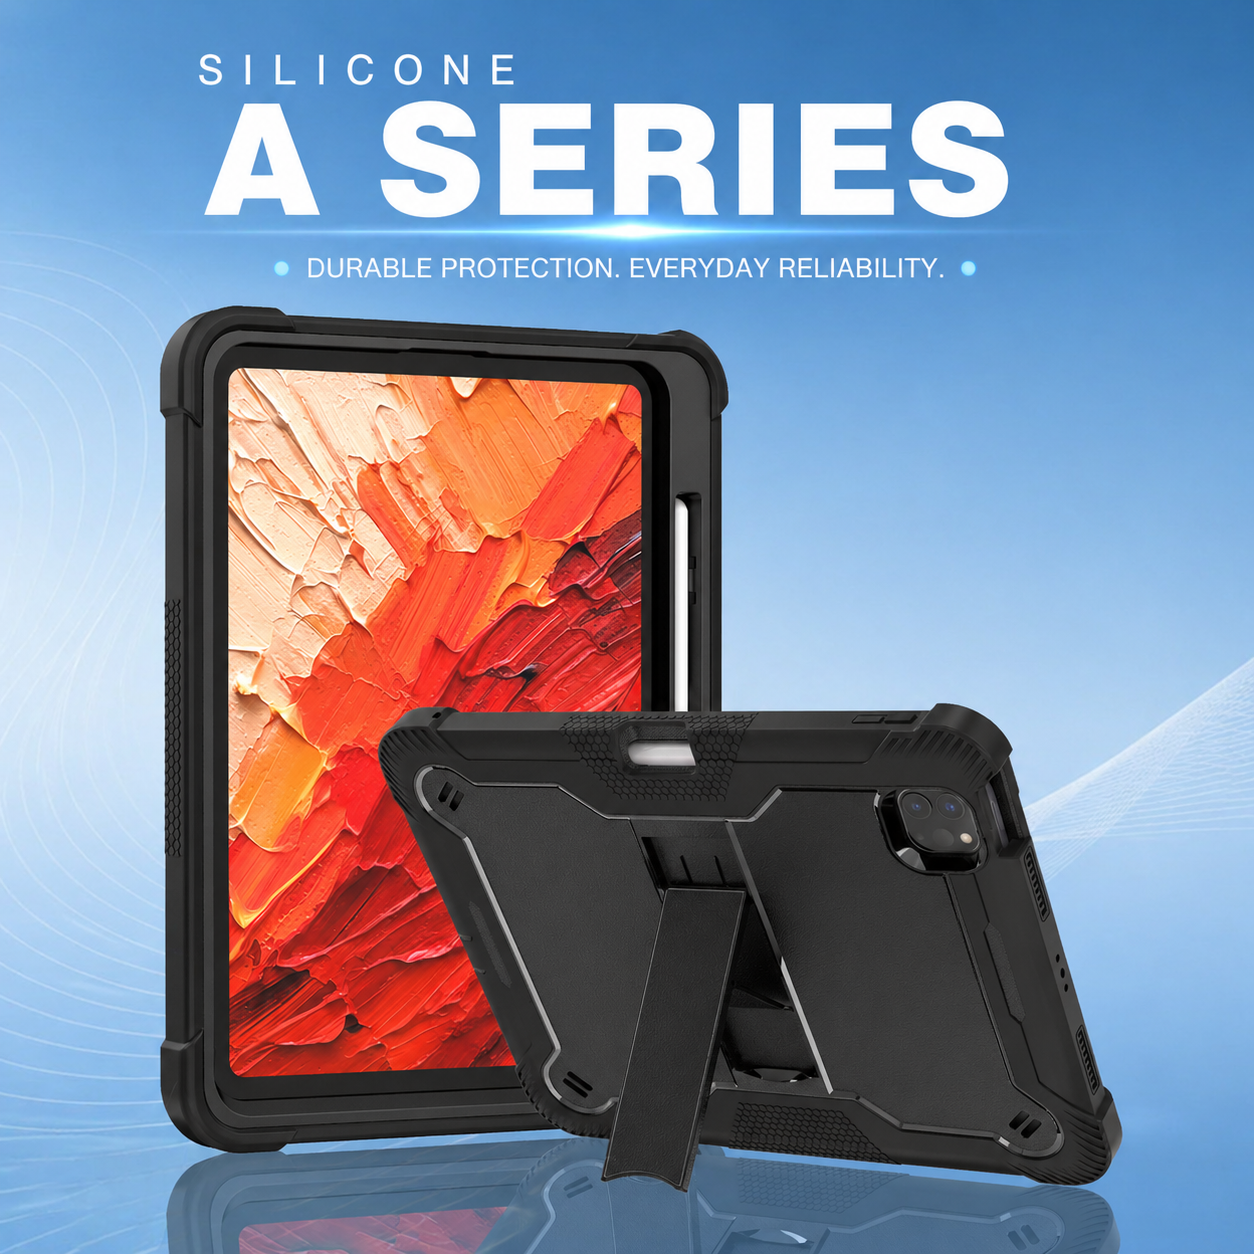
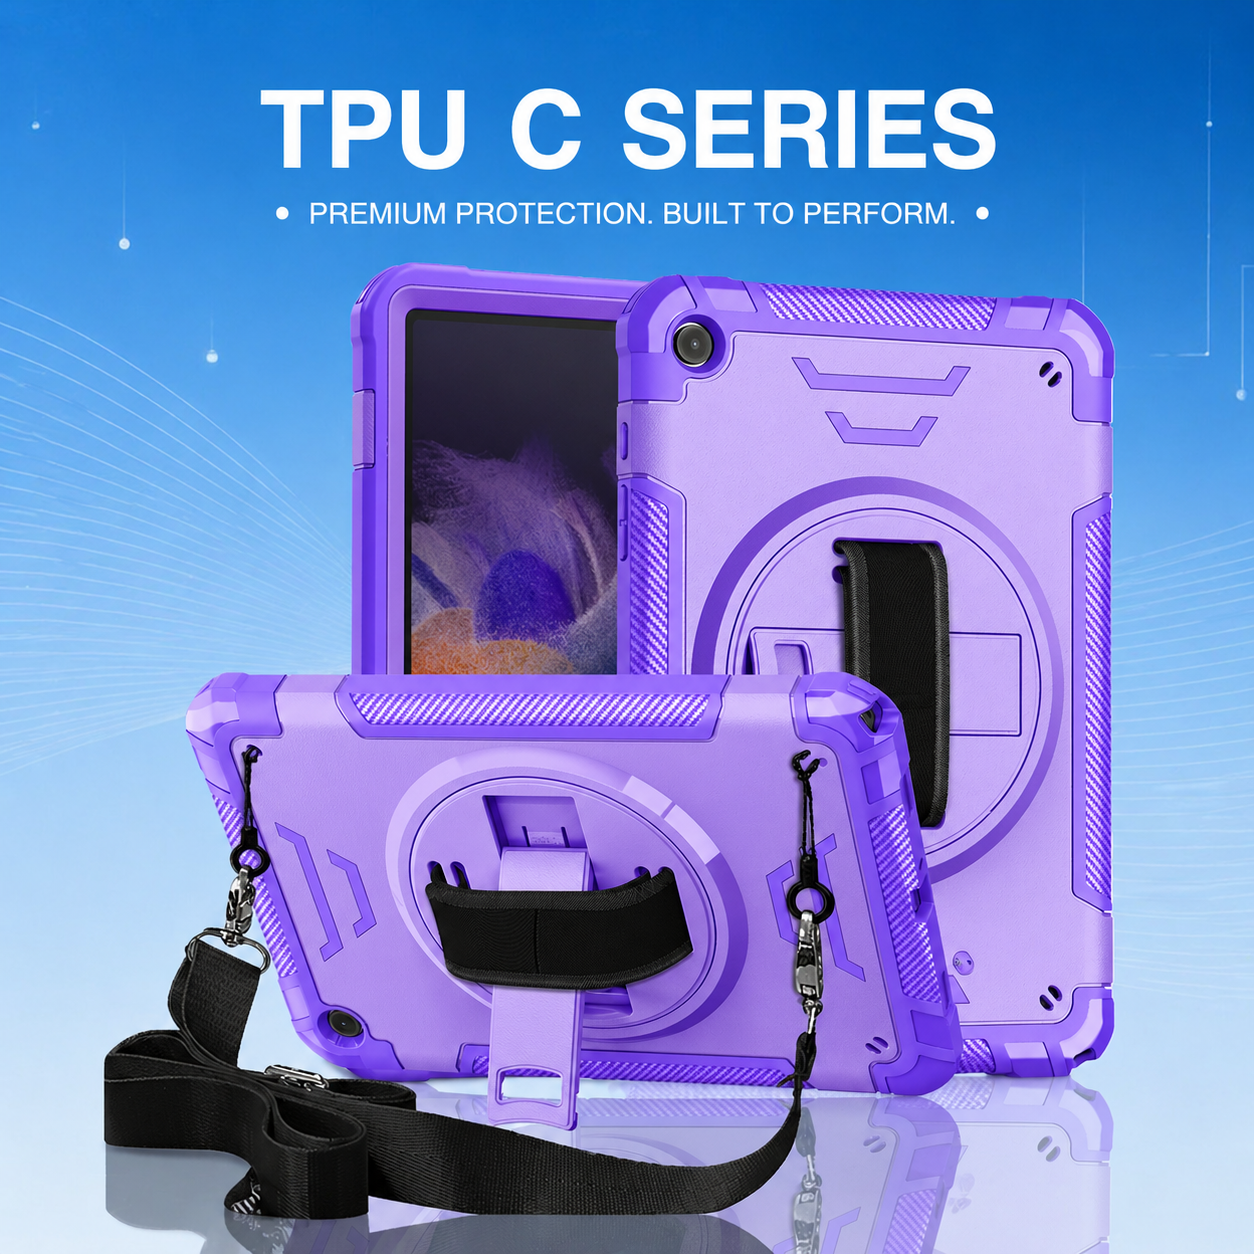
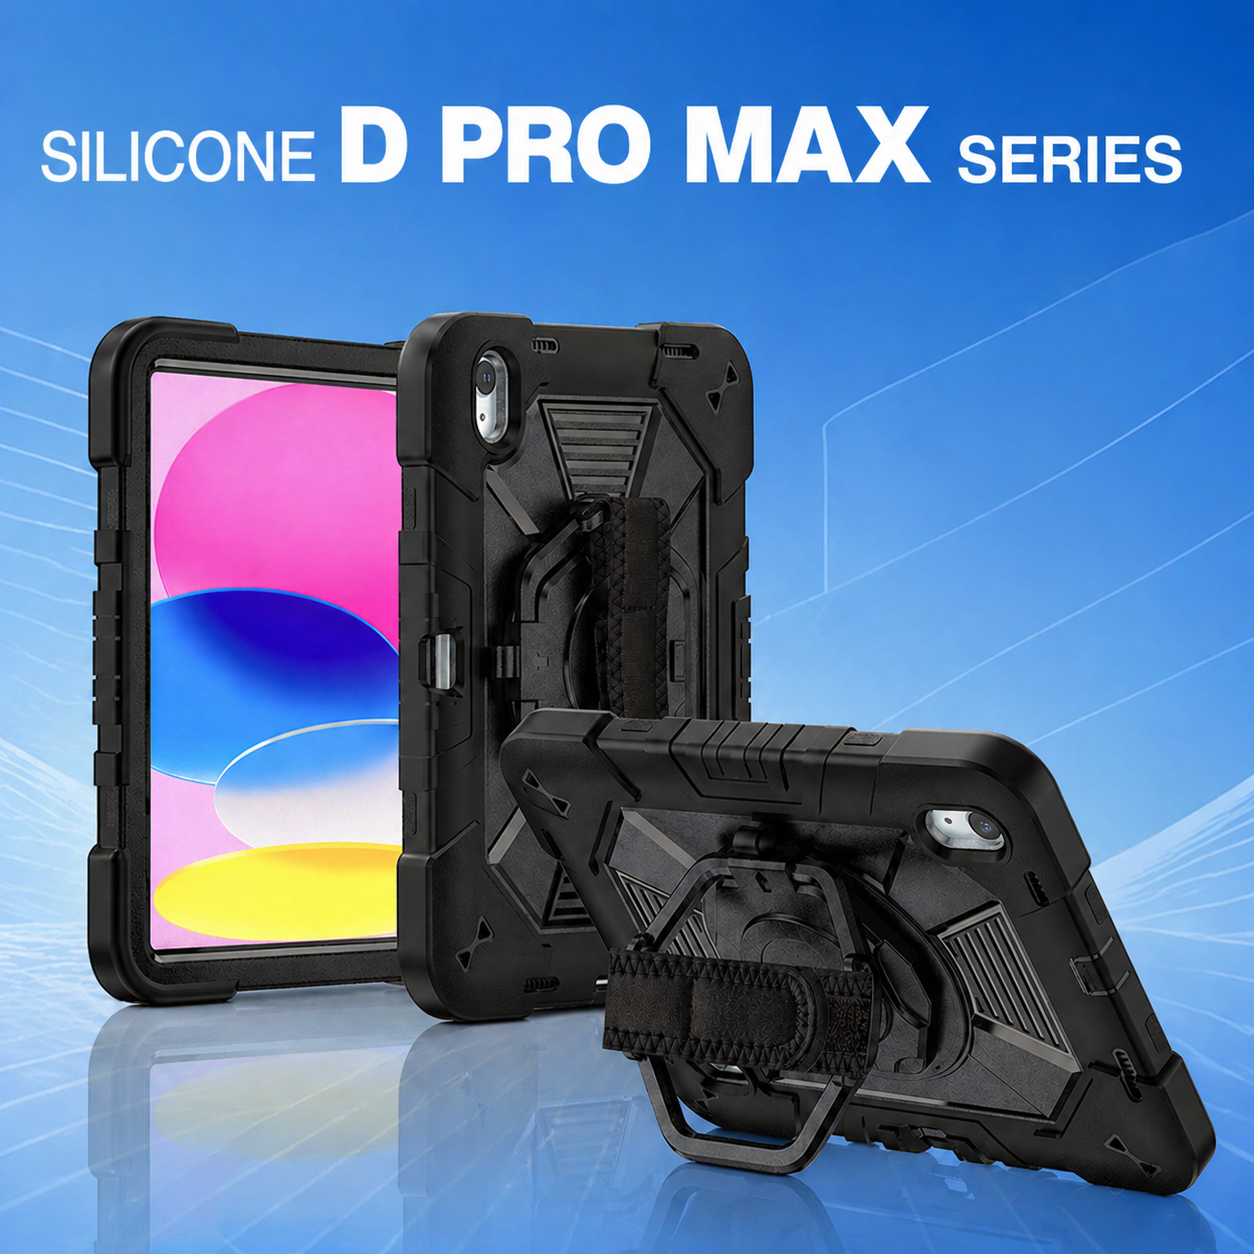
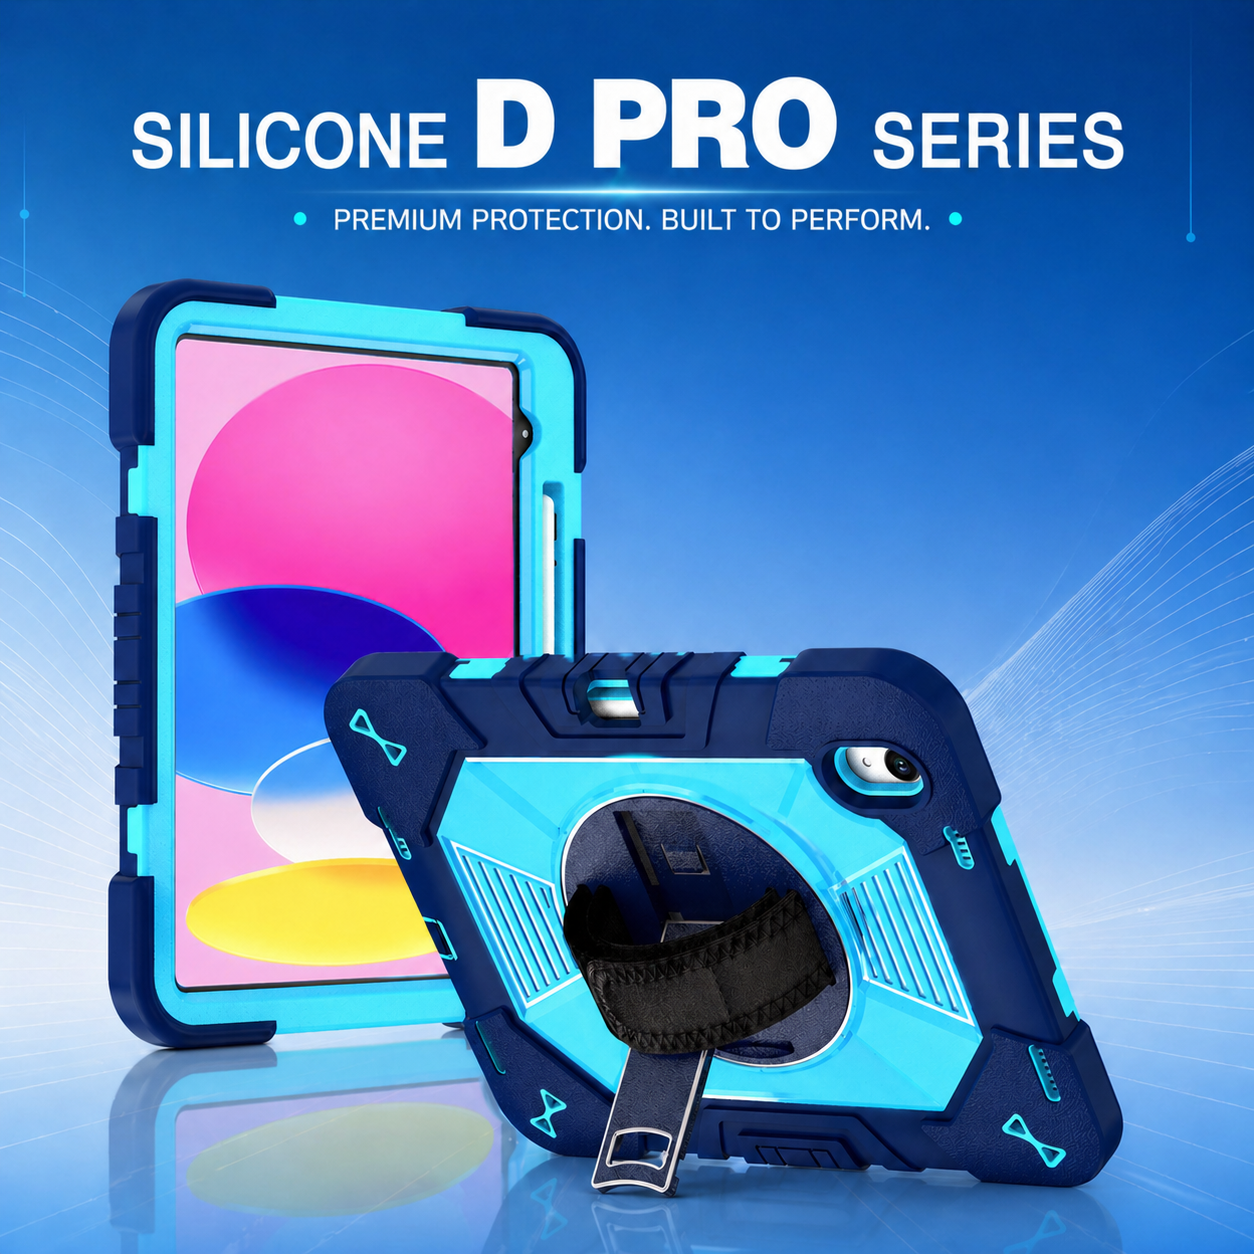
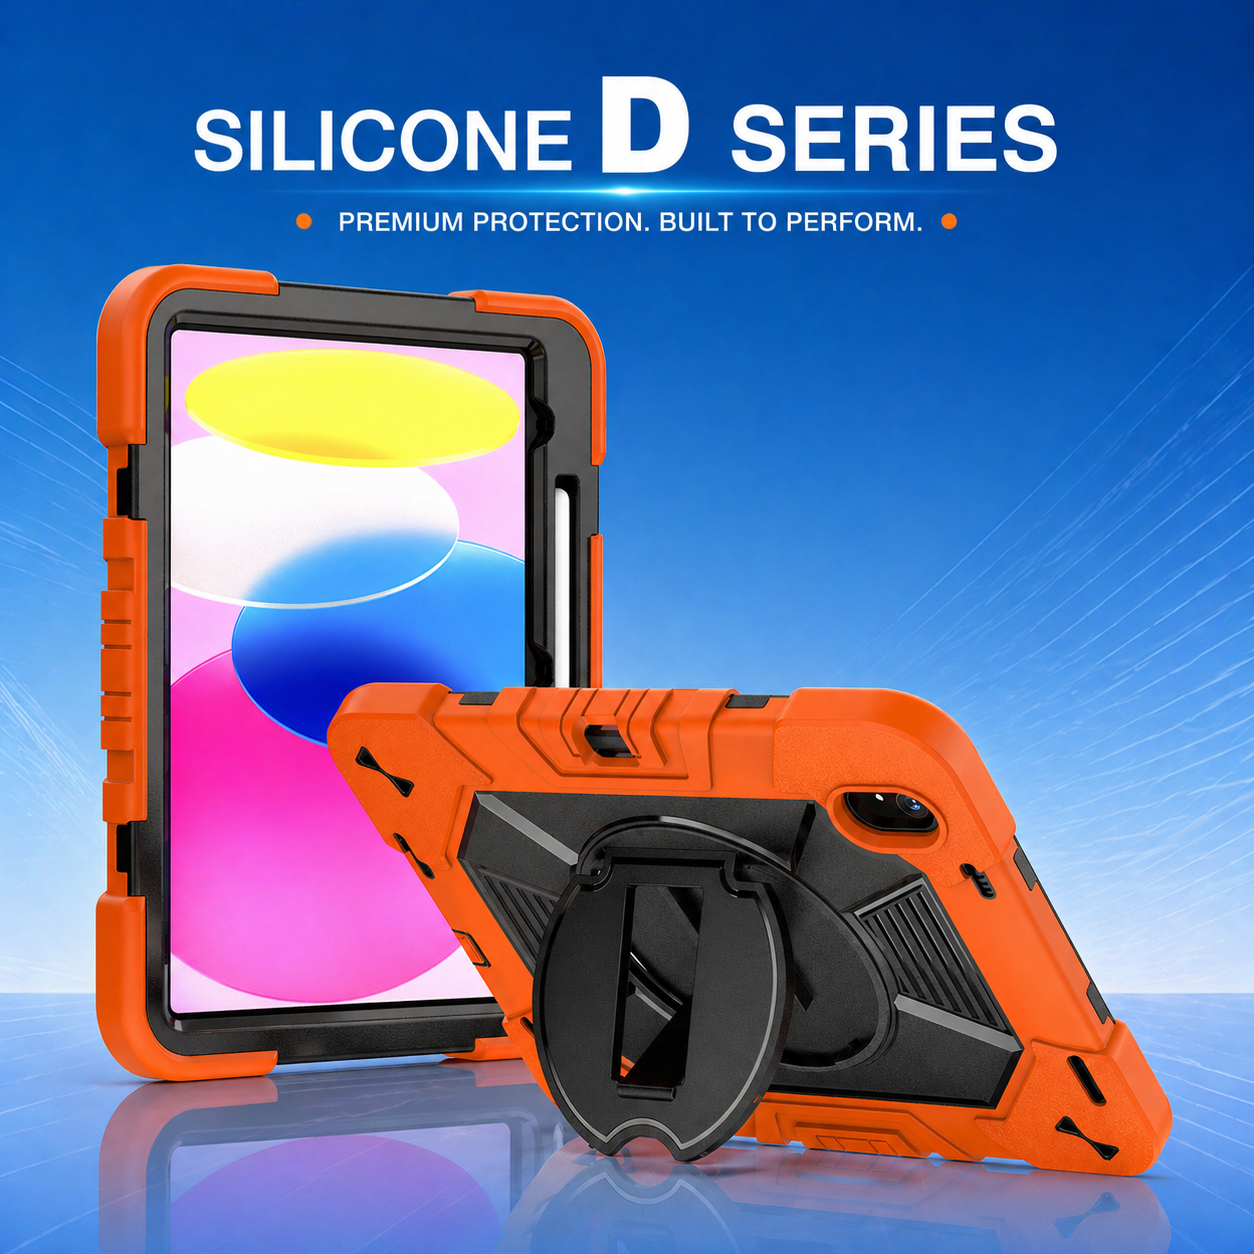
The best tough tablet protective shells use advanced material blends to absorb shocks and resist daily wear. Silicone PC hybrid tablet protective covers are a industry benchmark, balancing flexibility and rigidity.
Silicone and PC composite construction: Soft silicone inner layers absorb impact, while hard PC outer shells deflect sharp objects and direct blows.
Three-in-one layered protective structure: Adds a middle buffer frame to distribute impact force across the entire case, reducing pressure on tablet corners and screens.
Reinforced corner buffer design: Thickened corner bumpers absorb up to 90% of drop force, according to third-party drop test data.
For field service technicians and construction site operators, this level of protection prevents costly damage from 4-6 foot drops, a common hazard on job sites. Impact-absorbing tablet protective casings also reduce screen crack rates by up to 75% compared to basic tablet protective covers.
1.2 Environmental Resistance for Harsh Working Conditions
Beyond drops, industrial tablet cases must defend against dust, moisture, and slips that threaten device functionality in demanding settings. Drop slip dust resistant tablet cases for wholesale are designed to meet these multi-hazard needs.
Anti-slip surface texture: Textured side grips reduce accidental drops by 40% for warehouse operation staff handling devices with gloved hands.
Scratch-resistant outer shell: Protects tablet exteriors from scuffs caused by tools, equipment, and daily transport in work trucks.
Precise port and button cutouts: Sealed port covers block dust and liquid intrusion while maintaining full access to charging ports and volume controls.
Logistics workforce teams often use these cases in rain, snow, or dusty warehouse environments, where even small amounts of debris can disable a device. Reinforced tablet outer shells with IP54-rated dust resistance are ideal for these use cases.
2. Functional Features That Boost On-the-Job Usability
Protection alone isn’t enough—quality rugged tablet covers include ergonomic features that make devices easier to use in fast-paced work environments. These features directly impact worker efficiency and reduce fatigue during long shifts.
2.1 Built-In Support and Carrying Solutions
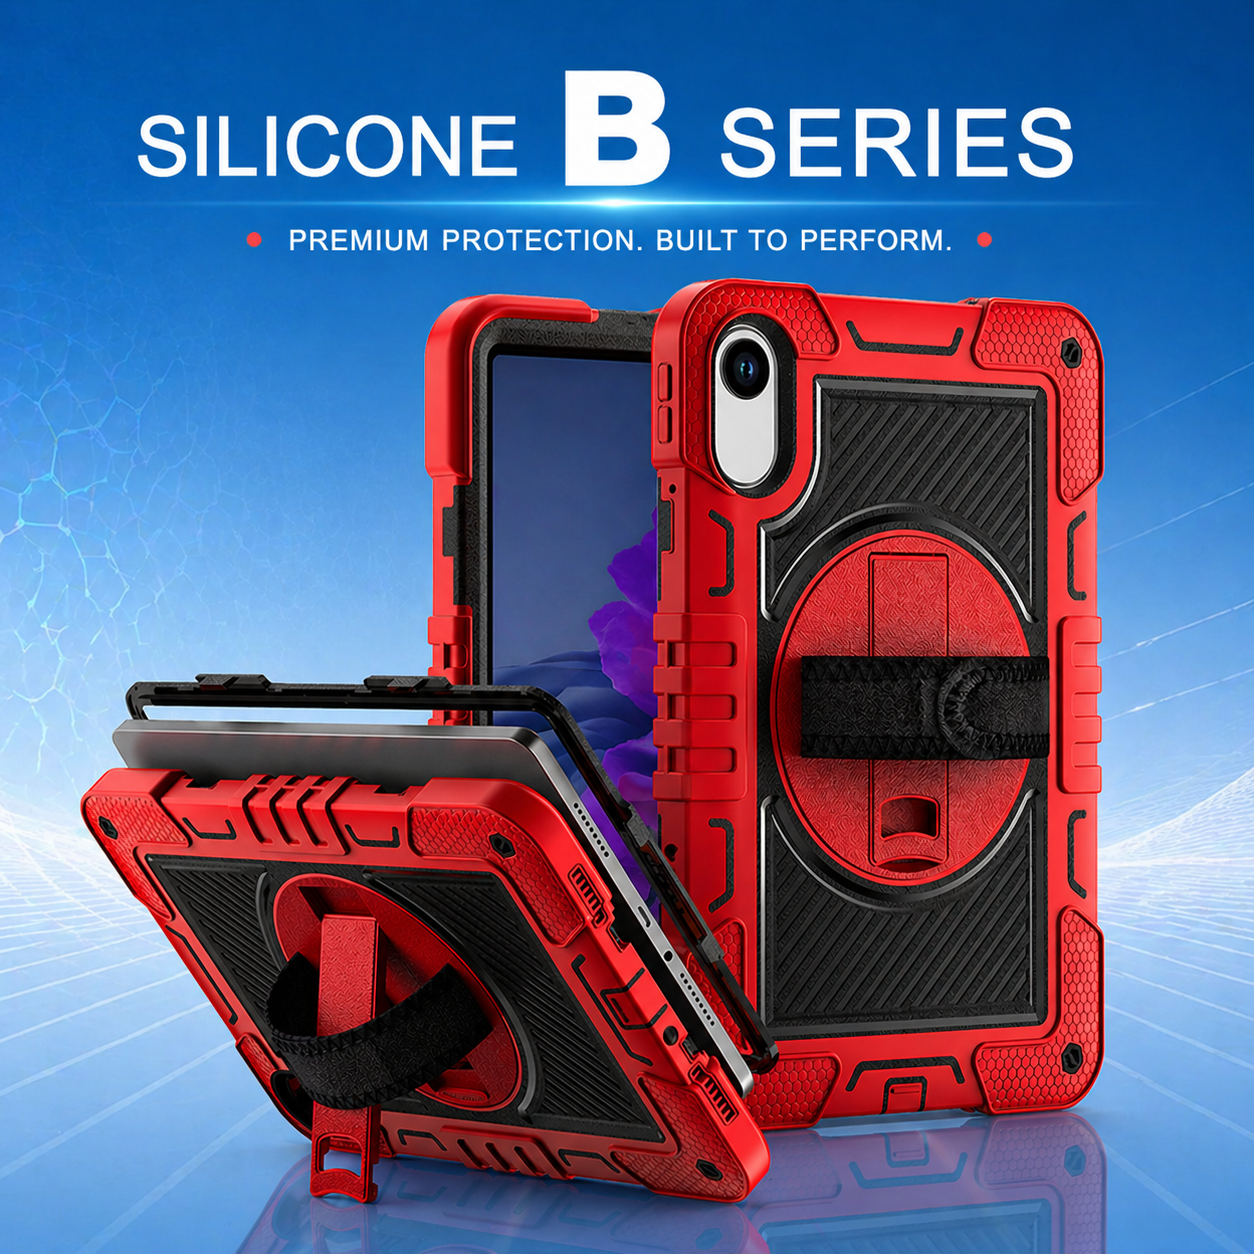
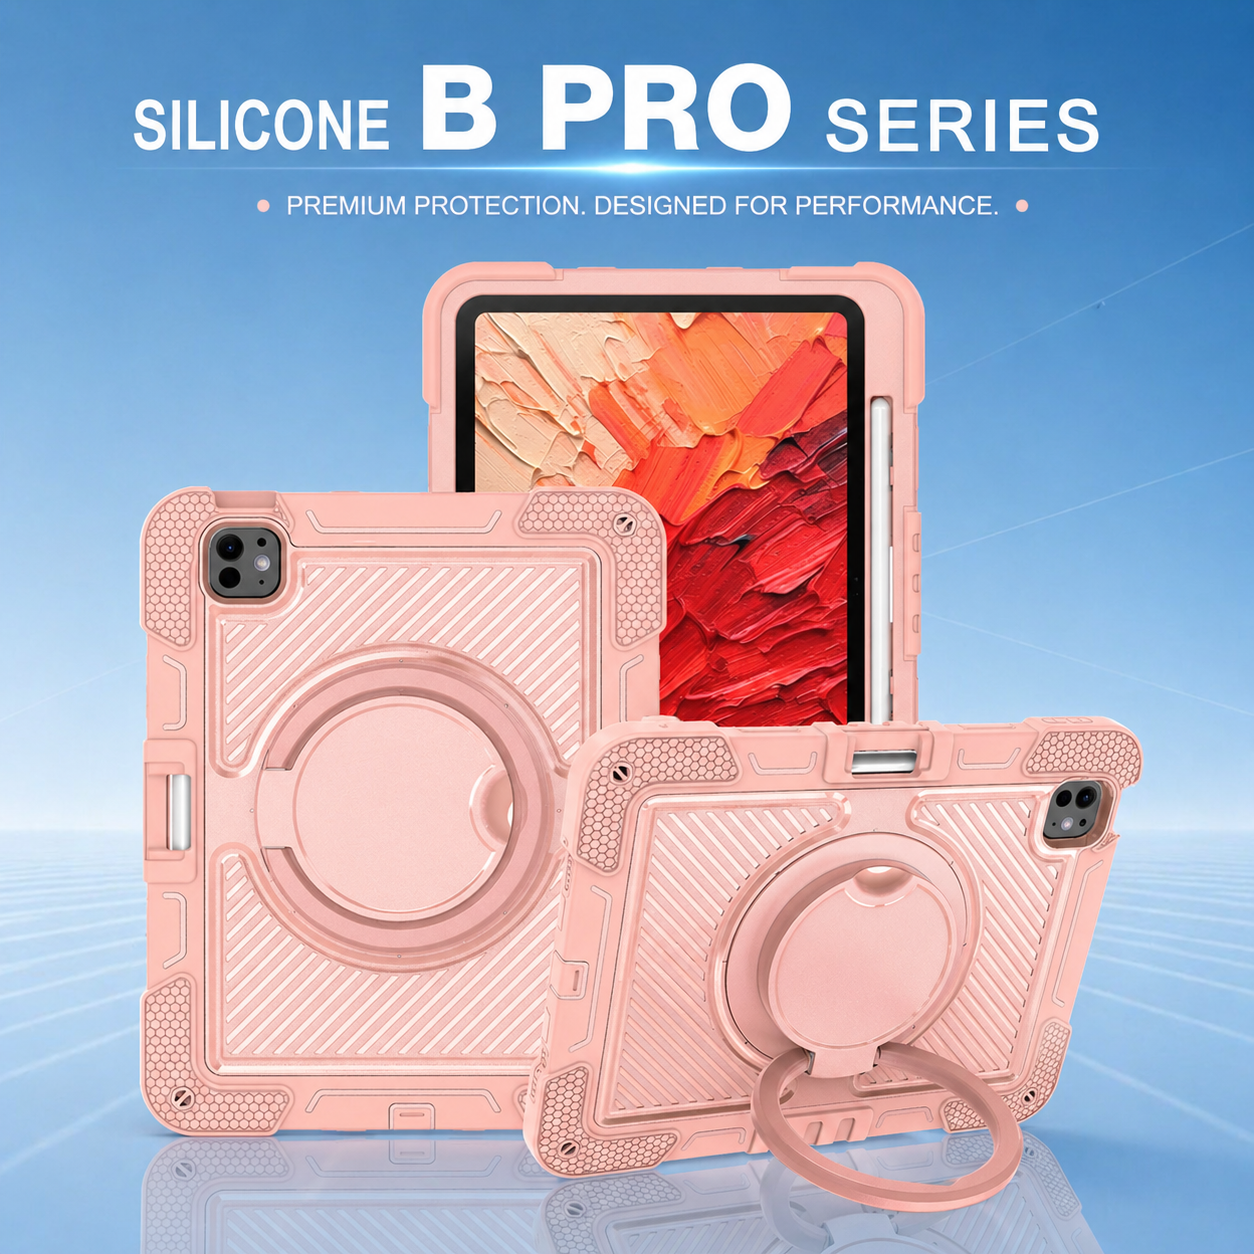
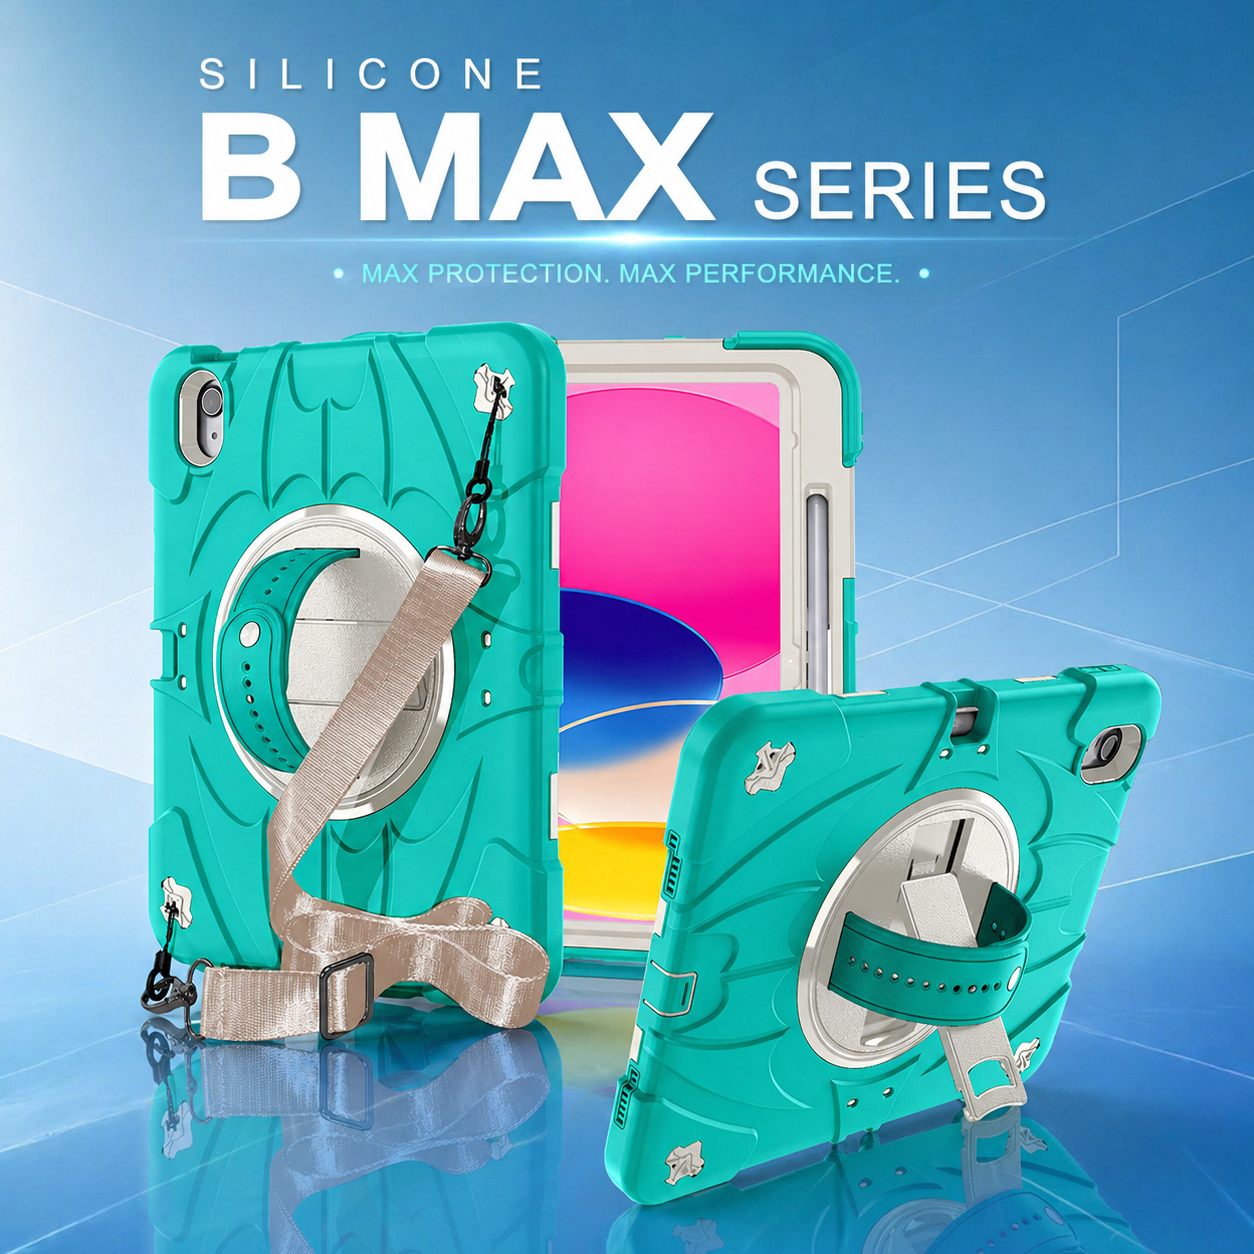
Hands-free support and comfortable carrying options are top requests from field workers and educators alike. Durable tablet cases with foldable stable kickstands and strap options deliver versatile functionality.
Stable foldable kickstand mechanism: Allows users to prop tablets at multiple angles for data entry, video calls, or training sessions, reducing neck strain for education institution educators.
Ergonomic hand grip structure: Adjustable hand straps on the back of the case let users hold tablets securely with one hand, leaving the other free to scan barcodes or take notes.
Optional widened adjustable shoulder strap: Distributes weight across the shoulder, making it easier for outdoor field workers to carry tablets for hours without discomfort.
Foldable kickstand tablet cases are especially popular in classroom settings, where teachers use them for interactive lessons and student presentations. Tablet cases with adjustable hand grip straps are a top choice for retail inventory teams.
2.2 Use-Case-Specific Design Add-Ons
Different industries require unique features tailored to their daily workflows. Three-in-one rugged tablet cases for field work often include specialized add-ons to meet niche needs.
Stylus holder slots: Keep digital pens within easy reach for construction site operators marking blueprints or healthcare staff updating patient records.
Mounting compatibility: Works with vehicle mounts, wall mounts, and forklift mounts for logistics teams needing hands-free access during transport.
Custom cutout options: Supports barcode scanners, RFID readers, and other device attachments used in warehouse operations.
For school students, classroom-oriented rugged tablet covers may include reinforced edges and non-toxic materials to withstand rough handling. Anti-slip textured tablet covers also reduce the risk of devices slipping off desks during class.
3. What B2B Buyers Expect From Tablet Case Suppliers
Finding the right tablet case supplier is just as important as choosing the right product. What B2B buyers expect from tablet case suppliers goes beyond product quality—it includes reliability, customization, and long-term partnership potential.
3.1 Manufacturing and Customization Capabilities
Suppliers with strong in-house capabilities can adapt to unique buyer needs and deliver consistent quality across large orders. Tablet case manufacturers with rich mould development experience stand out in this area.
Custom mould design: Can create cases for new tablet models within 30-45 days, helping e-commerce sellers stay ahead of market trends.
Branding options: Offers logo printing, color matching, and packaging customization to help wholesale distributors build their own brand identity.
Material flexibility: Can adjust silicone/PC ratios to meet specific impact resistance or cost requirements for different buyer segments.
For enterprise procurement managers, working with a supplier that can scale from small sample orders to bulk shipments ensures a smooth rollout across teams. Reliable suppliers also provide detailed material safety data sheets (MSDS) for all components.
3.2 Quality Assurance and Compliance Standards
Trustworthy suppliers back their products with verifiable testing and compliance certifications. This is especially critical for global foreign trade business buyers navigating different regional regulations.
Third-party testing: Provides MIL-STD-810G drop test reports, IP rating certificates, and RoHS compliance documents to prove product performance.
Batch quality control: Conducts 100% functional testing and 20% random drop testing for each production batch to reduce defect rates below 0.5%.
Warranty support: Offers 1-2 year product warranties and replacement services for defective units, reducing post-purchase risk for buyers.
Corporate IT deployment teams rely on these certifications to ensure devices meet company safety standards before rolling out to hundreds or thousands of employees.
4. Industry-Specific Rugged Tablet Case Use Cases
Rugged tablet cases serve diverse industries, each with unique priorities and pain points. Understanding these use cases helps buyers match products to their exact needs and helps sellers target high-demand markets.
4.1 Field and Industrial Applications
For field work and industrial settings, durability and functionality are non-negotiable. Field-ready tablet protective casings are built to withstand the toughest conditions.
Construction sites: Reinforced corner tablet bumper cases protect devices from falls, concrete impacts, and dust exposure for site managers and surveyors.
Field service: Three-in-one hybrid tablet protective cases with shoulder straps let technicians carry devices between job sites while keeping hands free for repairs.
Logistics and warehousing: Silicone PC composite tablet cases with hand grips and barcode scanner cutouts streamline inventory management and order fulfillment.
Bulk procurement of rugged tablet cases for education sectors also requires industrial-level durability, as devices are used by hundreds of students across multiple years. Classroom cases often include antimicrobial coatings to support school health policies.
4.2 Commercial and Educational Applications
Office, retail, and education environments have different needs than industrial settings, focusing more on usability and brand consistency.
Retail: Scratch-resistant tablet housings with kiosk mode compatibility work well for point-of-sale systems and customer self-service stations.
Education: Classroom-oriented rugged tablet covers with thick bumpers and screen protectors reduce damage from drops, spills, and daily student use.
Corporate enterprise: Sleek, durable tablet bumper covers with company branding support professional client presentations while protecting devices during travel.
For retail wholesale distributors, stocking a range of cases for different use cases helps capture a broader customer base. Enterprise sourcing of durable tablet protective housing often involves multi-year contracts with consistent pricing and delivery timelines.
5. How to Evaluate and Select the Right Supplier
With so many suppliers in the market, narrowing down options can be overwhelming for startup founders, small business owners, and enterprise teams alike. These evaluation criteria help identify partners that deliver long-term value.
5.1 Key Evaluation Metrics for Suppliers
Before committing to a partnership, verify these core supplier capabilities to avoid costly mistakes down the line.
Production capacity: Can they handle 10,000+ unit monthly orders without delaying delivery timelines?
Sample policy: Do they offer free or low-cost samples so you can test product quality before placing bulk orders?
Trade experience: Reliable tablet case suppliers for global foreign trade business have 5+ years of export experience and understand international shipping rules.
Communication: Do they provide dedicated account managers and respond to inquiries within 24 hours in your time zone?
For e-commerce sellers, fast sample turnaround and flexible MOQ (minimum order quantity) terms are critical for testing new products and scaling quickly. Small business owners may prioritize lower MOQs to reduce upfront inventory costs.
5.2 Cost vs. Value: Finding the Right Balance
While price is always a consideration, choosing the cheapest option often leads to higher long-term costs from product failures and returns.
Calculate total cost of ownership (TCO): Include product cost, shipping, warranty coverage, and expected replacement frequency to compare true value.
Ask for client references: Speak with other B2B buyers in your industry to learn about their experience with the supplier’s product quality and customer service.
Review product testing data: Request detailed test reports for drop resistance, dust protection, and material durability to validate performance claims.
According to industry data, investing in high-quality rugged tablet cases reduces total device ownership costs by 30-40% over 3 years by cutting replacement and repair expenses.





+86 13422271740

info@tongmeitech.com

No. 34, Mashe Section, Guihe Road, Lishui Town, Foshan, Guangdong, China