- 1
- BLACKL
- TABLETAPPLE iPad Mini 8NEW iPad A16(2025) iPad 10.9" 10th (2022) iPad 10.2" (7th/8th/9th) iPad Air 13" (M2/M3/M4)(2024/2025/2026)NEW iPad Air 11" (M2/M3/M4)(2024/2025/2026)NEW iPad Mini 8.3" (A7 Pro/6th Gen) iPad Pro13"(M4/M5)(2024/2025) iPad Pro11"(M4/M5)(2026) iPad 9.7" (5th/6th Gen) iPad Pro 12.9"(2018-2022) iPad Pro 11"(2018-2022) iPad 9.7"(2th/3th/4th) iPad Air 10.9"(4th/5th Gen) iPad Mini 7.9"(4th/5th Gen)SAMSUNG Galaxy Tab A11 Galaxy Tab A11 Plus Galaxy Tab S11 Galaxy Tab S12 PlusNEW Galaxy Tab S12 UltraNEW Galaxy Tab A9+ Galaxy Tab A9 Galaxy Tab A8 Galaxy Tab A7 Galaxy Tab A7 Lite Galaxy Tab S11 Ultra/S10 Ultra/S9 Ultra/S8 Ultra Galaxy Tab S10+/S9+/S9 FE+ Galaxy Tab S10Lite/S10 FE/S9 FE/S9 Galaxy Tab S8+/S7+/S7 FE Galaxy Tab S8/S7 Galaxy Tab S6 lite Galaxy Tab A10.1 Galaxy Tab A8.4 Galaxy Tab A8.0 Galaxy Tab S10 FE+LENOVO iDea tab 11/Tab K11 Gen 2 /Xiaoxin Pad 11 2025 Lenovo Tab K9 (Tab One) 2025 Lenovo Tab M10 10.1"(2025) Lenovo Tab M10 Plus 10.6" (3rd Gen) Lenovo Tab M10 HD 10.1" (3rd Gen) Lenovo K10/M10 Plus 10.3" (2nd Gen) Lenovo Tab M10 HD 10.1" (2nd Gen)XIAOMI Redmi Pad 2 9.7 InchNEW Xiaomi Pad8/8Pro 11.2" Redmi Pad2/Pad2.4G Xiaomi Pad 6/6 Pro 11" Redmi Pad 10.61" Redmi Pad Se 11" Redmi pad Se 4G 8.7" Xiaomi Pad7/7 Pro 11.2" Redmi Pad Pro/Xiaomi Poco Pad/Redmi Pad2 Pro 12.1HUAWEI Huawei Matepad Se 10.4" Huawei Matepad 11" Huawei Matepad 11.5" Huawei Matepad SE 11" Huawei Matepad T8 8" Huawei Matepad T10 9.7"
- CATEGORIES

How to Choose the Right Tablet Protective Cases for Wholesale and Business Use
In 2026, the global commercial tablet market is projected to grow by 8.3%, driving surging demand for reliable protection solutions. For e-commerce sellers and B2B buyers, finding the right tablet case wholesale partner directly impacts profit margins, customer satisfaction, and long-term business growth.
This buyer’s guide breaks down everything you need to know about sourcing bulk tablet protection cases, from supplier vetting to product specification matching.
1. Assess Your Business Needs Before Sourcing
Before reaching out to any supplier, define your core requirements to avoid costly mismatches.
1.1 Identify Target Industry Use Cases
Different industries demand distinct levels of protection and functionality. Align your product selection with end-user scenarios:
Education & Schools: Durable tablet covers with reinforced corners for K-12 and higher education device fleets
Warehouse & Logistics: Heavy duty tablet protection resistant to drops, dust, and moisture
Healthcare: Protective tablet enclosures that are easy to sanitize and compatible with medical carts
Corporate: Slim, professional tablet device covers for employee device programs
tablet cases for education and schools/行业定制平板保护套采购指南
1.2 Match Product Types to Device Models
Commercial deployments often involve mixed device fleets. Confirm compatibility with popular models:
Apple iPad (10th gen, iPad Pro, iPad Air)
Samsung Galaxy Tab S9, Tab Active series
Lenovo Tab M10, ThinkPad Tablet
Amazon Fire HD 10, Fire Max 11
Xiaomi Pad 6 series
Look for suppliers offering device-specific compatibility and precise model-specific cutouts for cameras, buttons, and ports.
alt: tablet cases for education, warehouse, healthcare, and corporate use
2. Evaluate Tablet Protective Case Wholesale Suppliers
Choosing the right supplier is as critical as selecting the right product. Vet potential partners across multiple dimensions.
2.1 Key Supplier Qualifications to Verify
Not all tablet case wholesalers are created equal. Prioritize partners with:
5+ years of experience in B2B tablet protection supply
ISO 9001 quality management certification
Compliance with RoHS, REACH, and FCC standards
In-house design and engineering teams for custom projects
2.2 Factory Direct vs. Trading Company Comparison
Tablet case factory direct wholesale offers unique advantages, but trading companies may suit smaller buyers:
| Factor | Factory Direct | Trading Company |
|---|---|---|
| Pricing | 15-25% lower | 10-15% markup |
| MOQ | Higher (500-1000pcs) | Lower (100-200pcs) |
| Customization | Full OEM/ODM capabilities | Limited customization |
| Lead Time | 25-40 days | 7-15 days (stock items) |
For large-scale bulk tablet cases for business orders, working directly with an OEM tablet protective case manufacturer delivers the best long-term value.
3. Prioritize Protection Features and Build Quality
The core value of any tablet safety case is its ability to prevent damage. Evaluate construction and protective features carefully.
3.1 Critical Protective Specifications
Look for these key protective tablet case structure features:
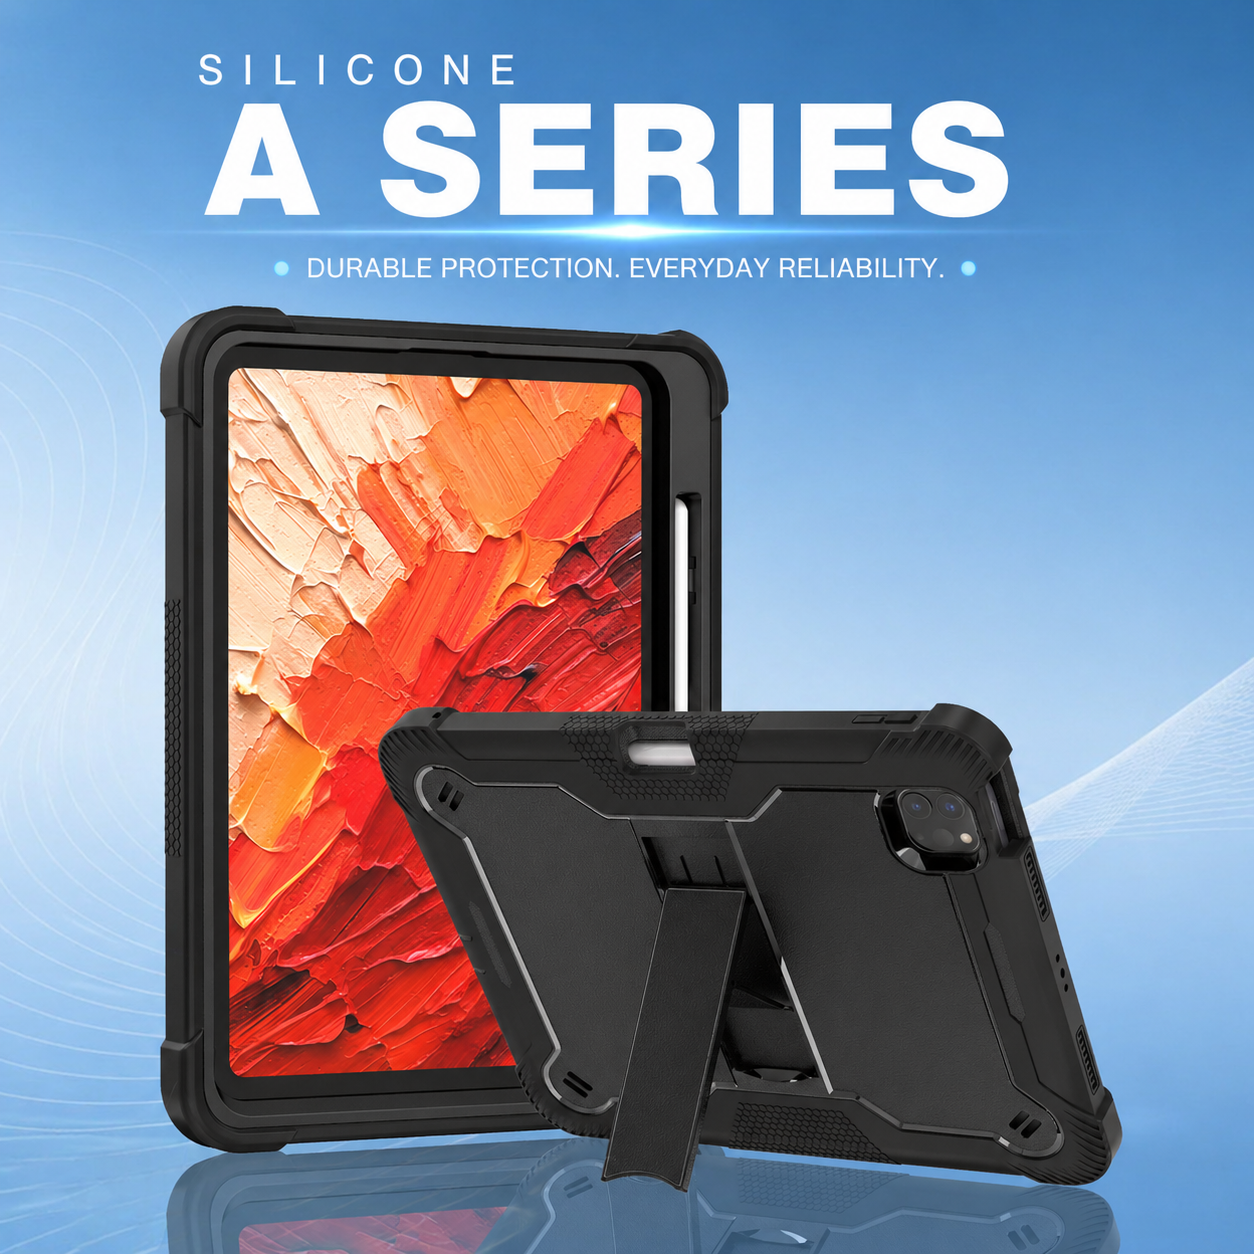
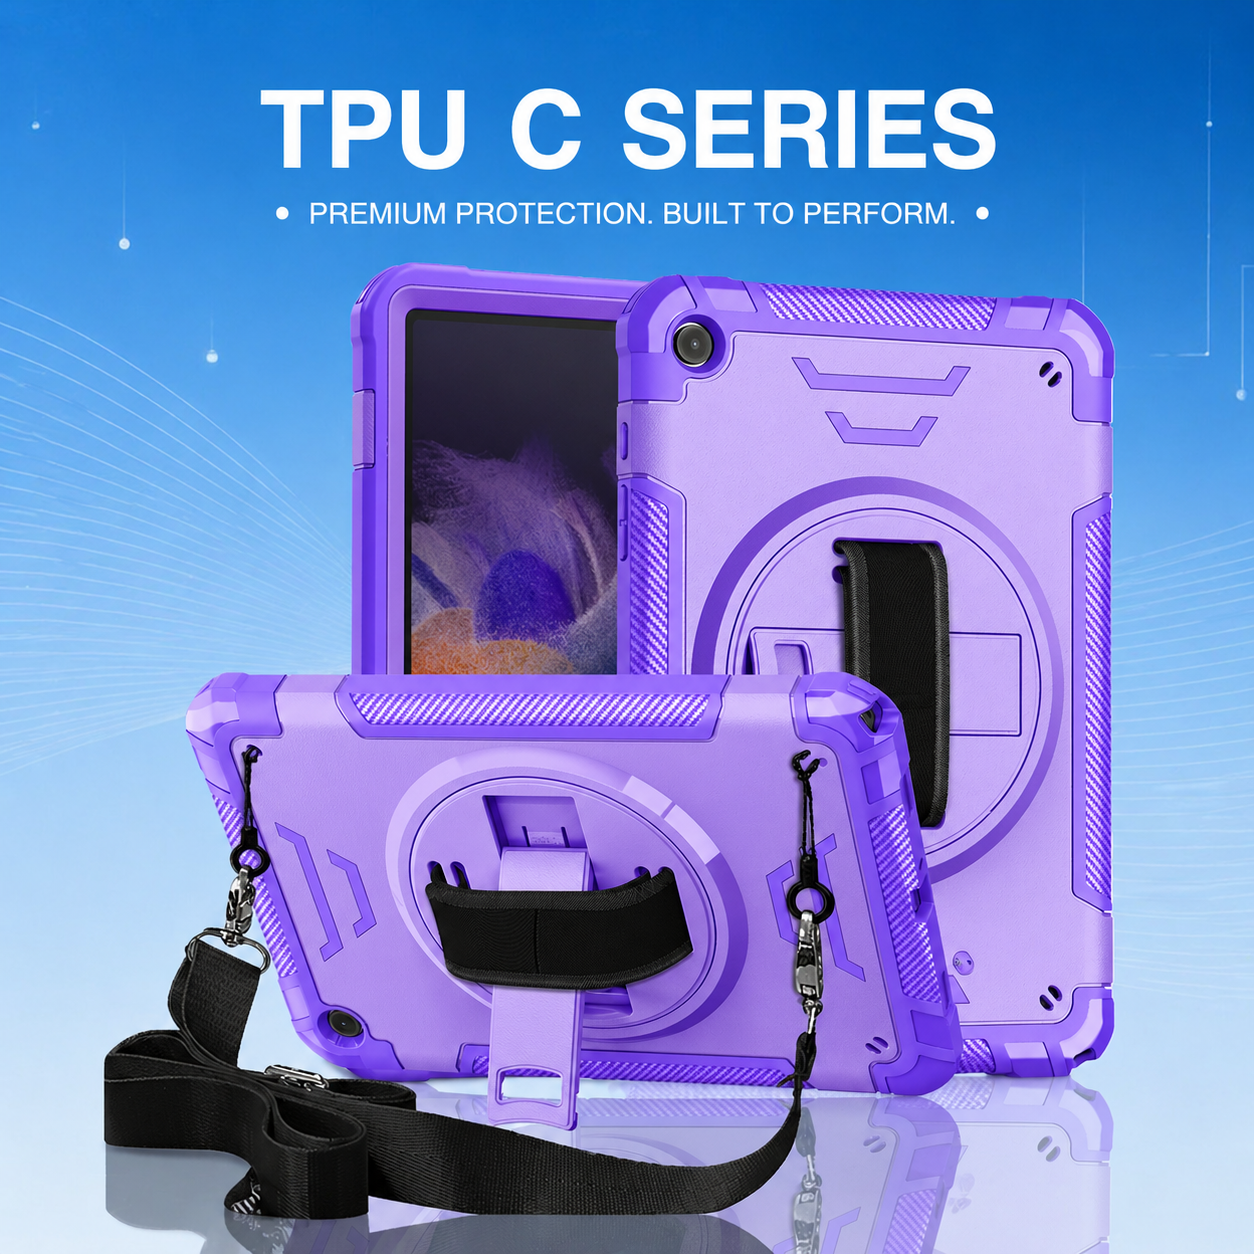
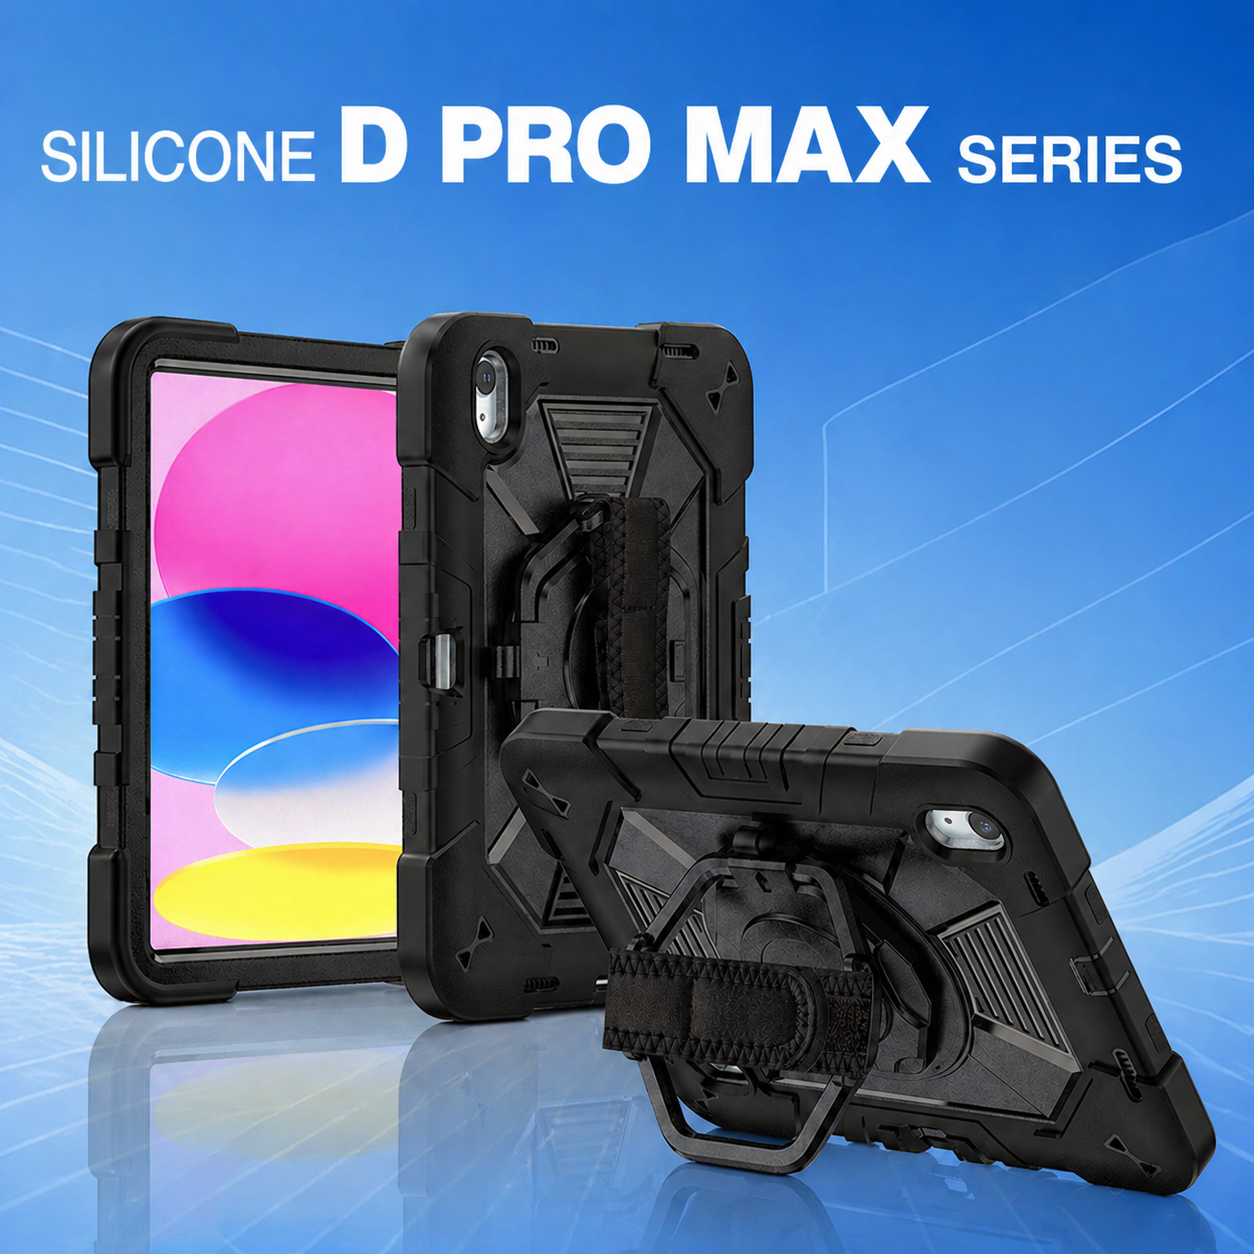
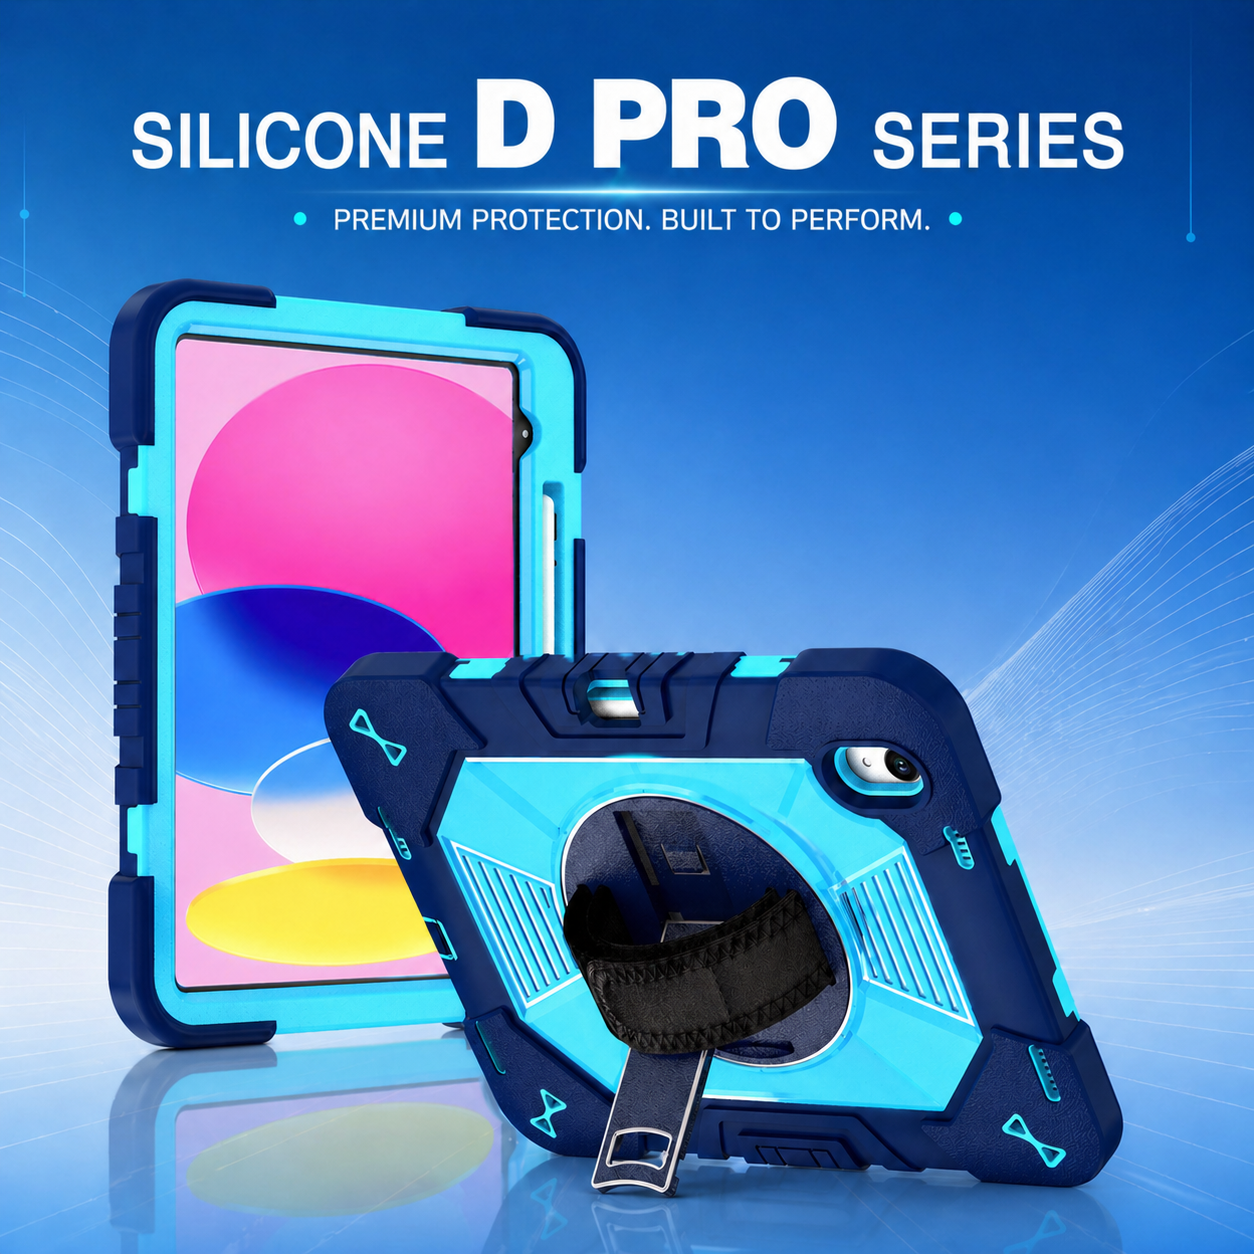
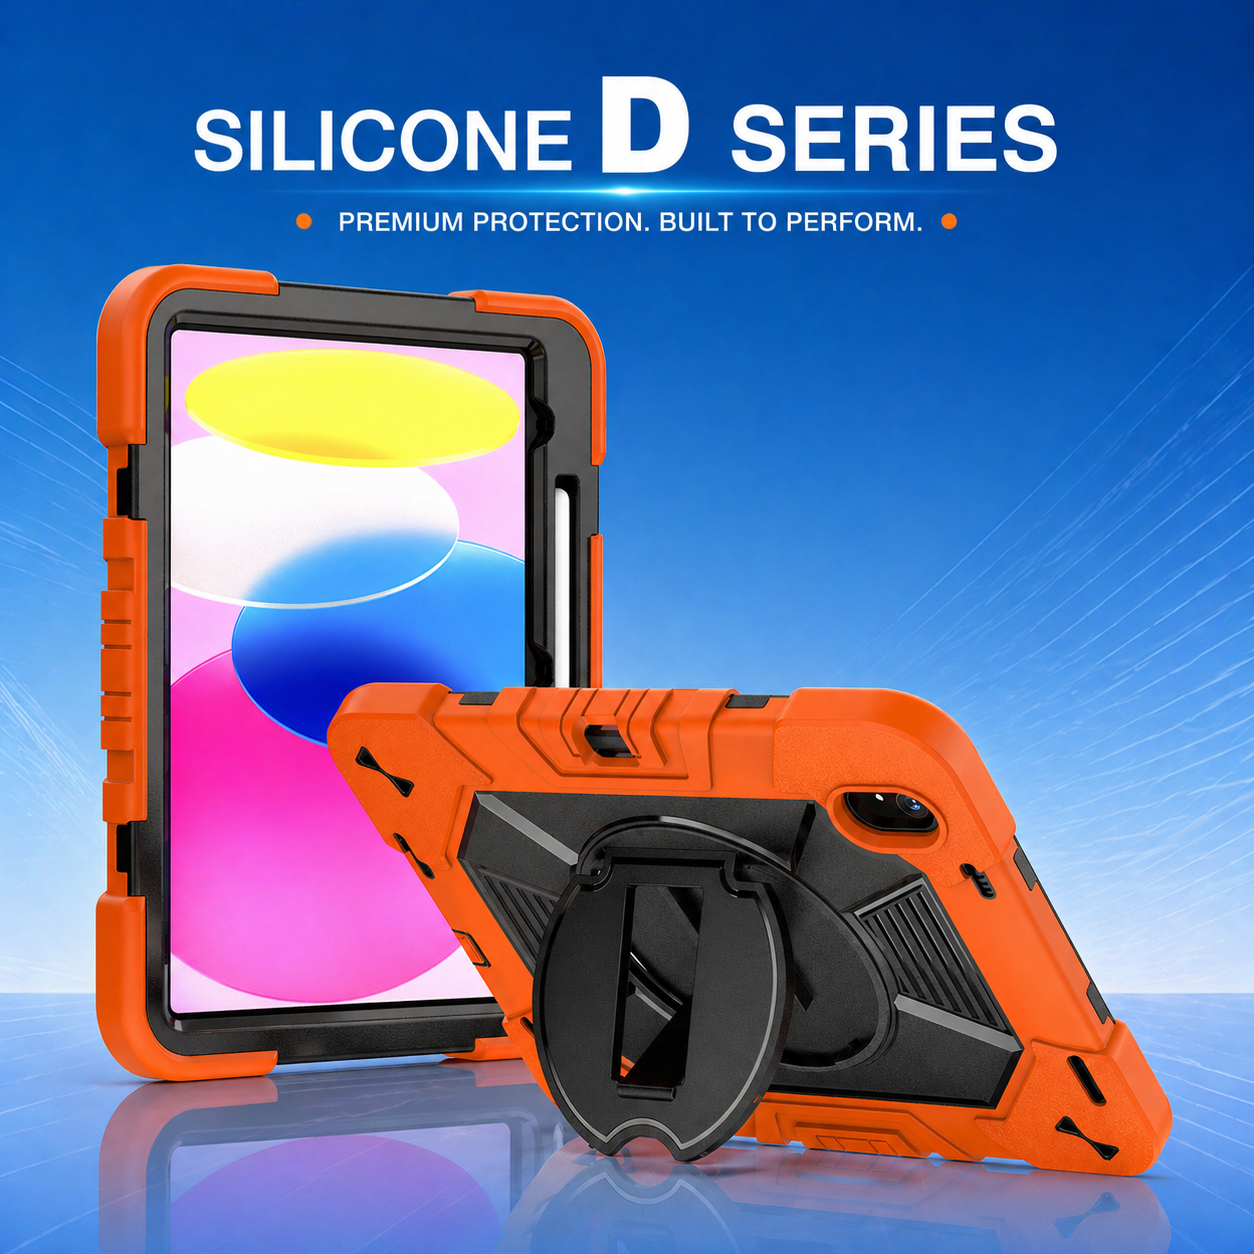
Three layer protective design: Inner soft TPU, middle shock-absorbing layer, outer hard PC shell
Reinforced protective corners: Air-cushion technology for drop impact absorption
Shock absorbing outer shell: High-density silicone or TPU material
Anti slip surface: Textured grip to reduce accidental drops
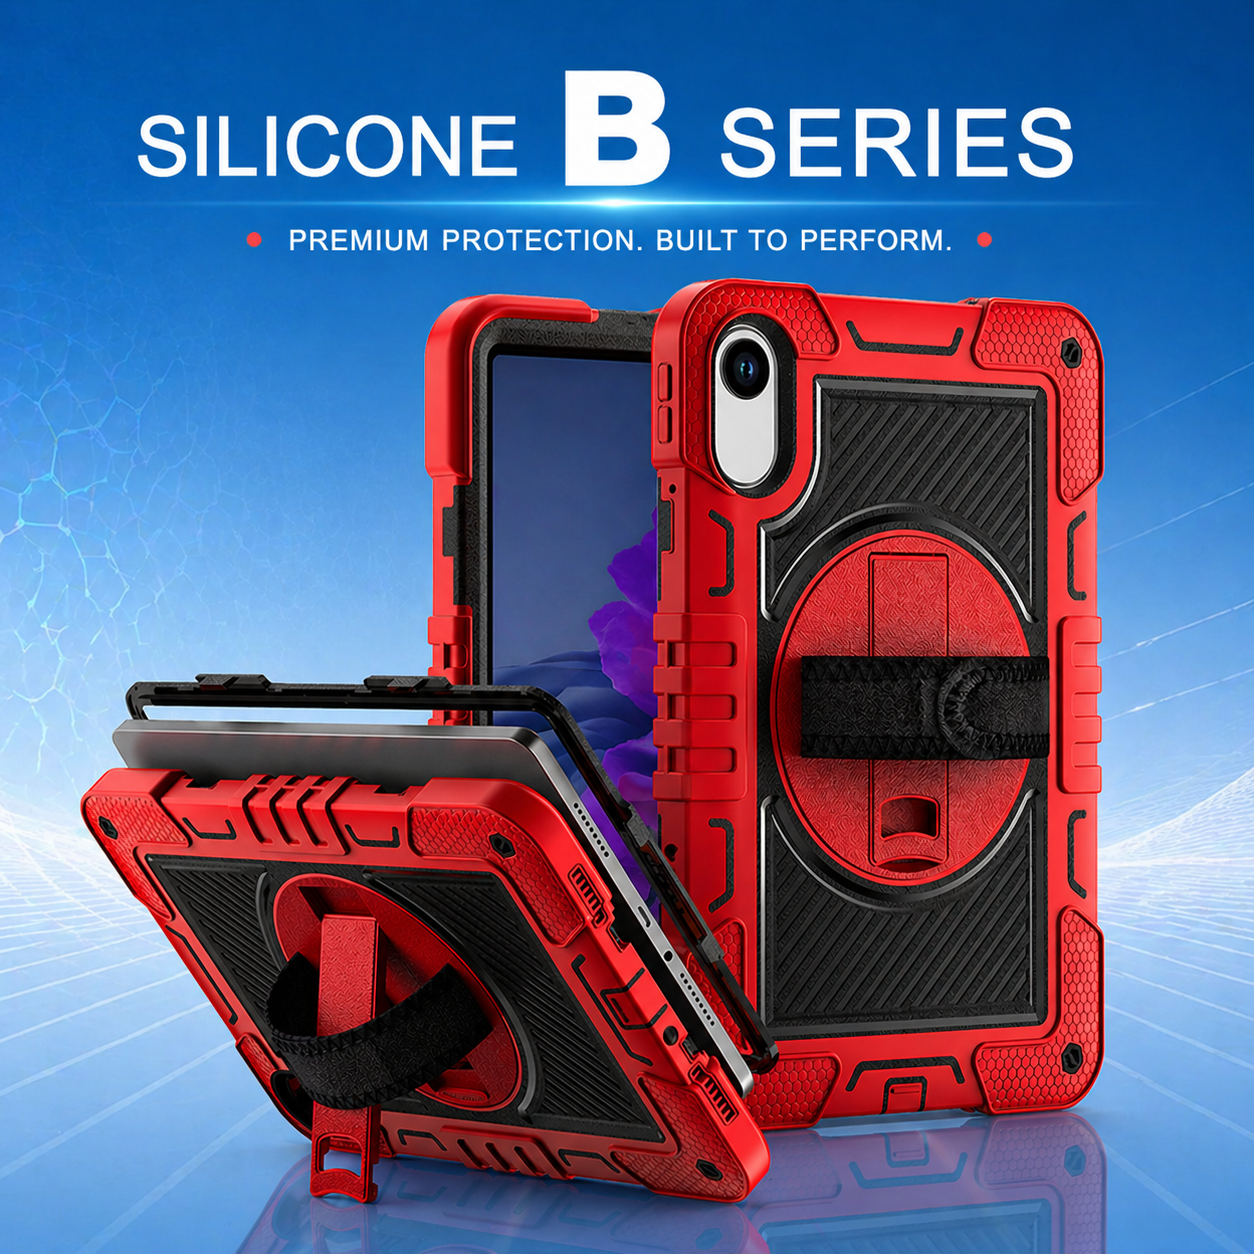
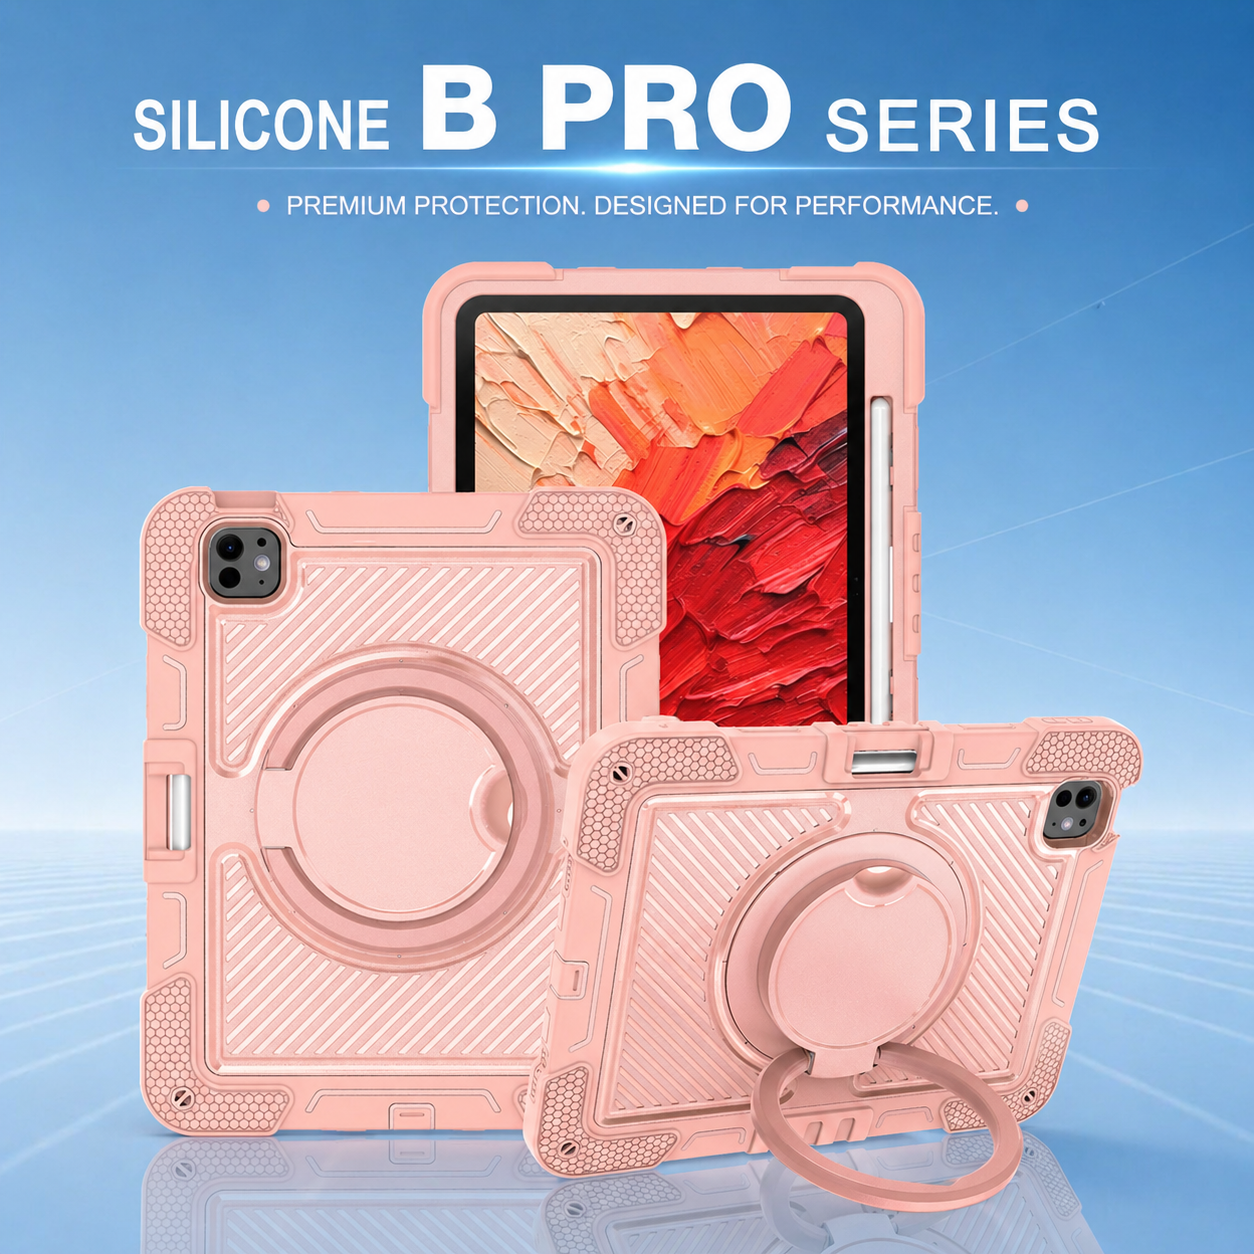
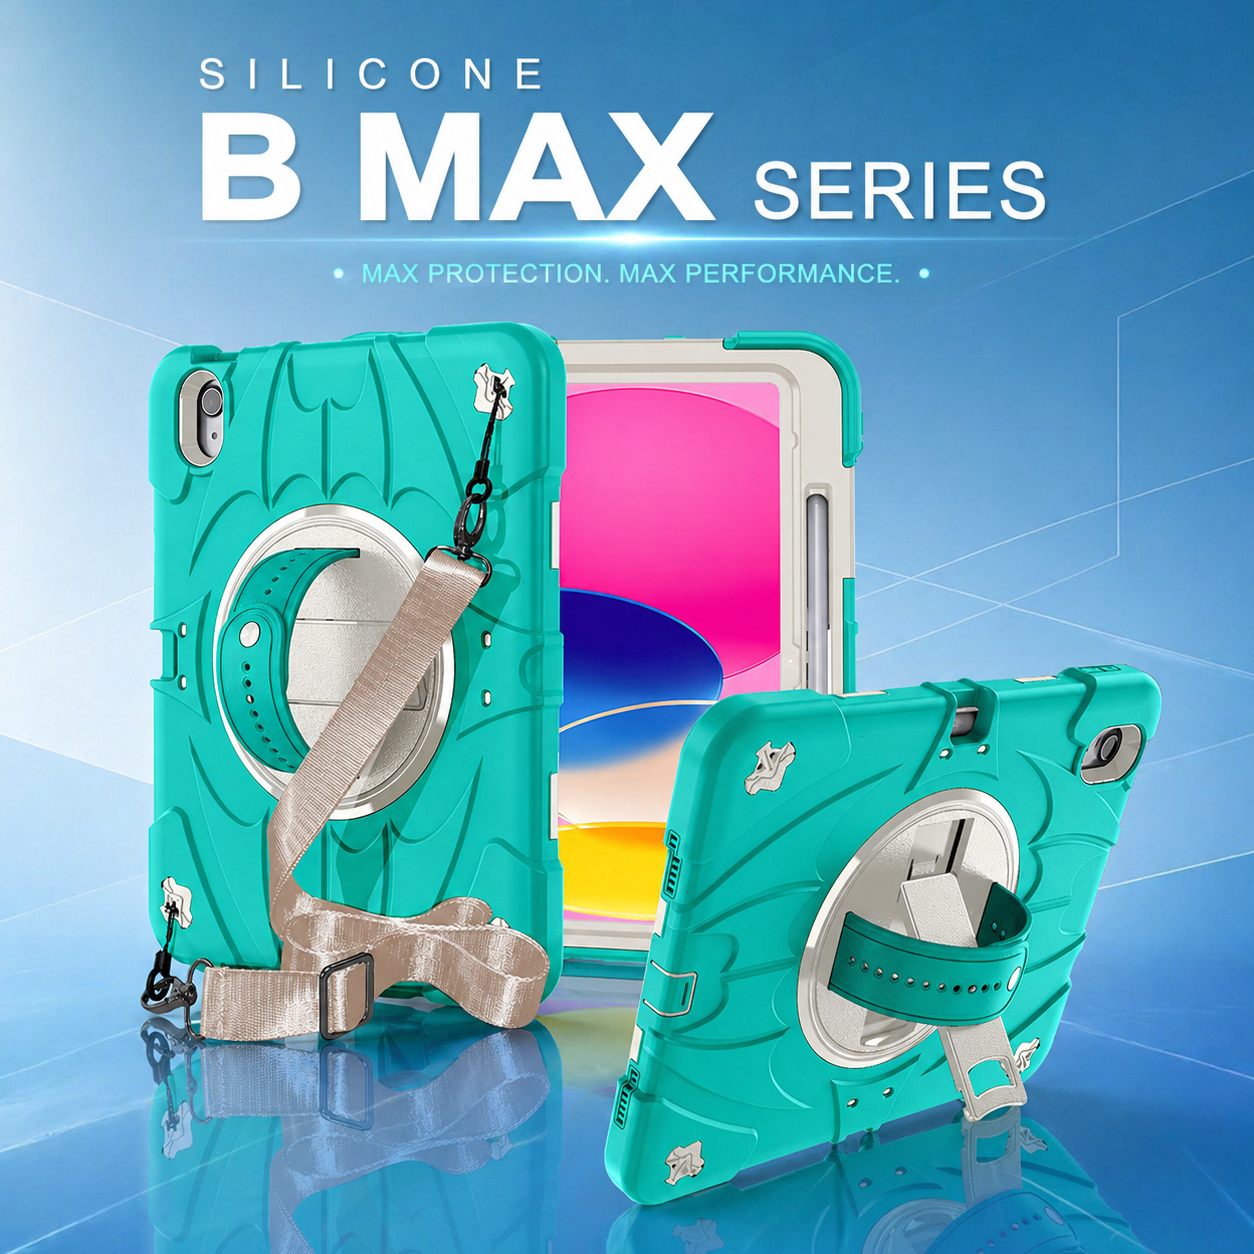
Shockproof silicone tablet cases with silicone and PC construction are the most popular choice for commercial applications.
3.2 Functional Features for Commercial Use
Beyond basic protection, consider features that boost productivity:
Foldable multi angle kickstand for hands-free viewing
360 degree rotating stand for landscape/portrait switching
Adjustable hand strap for secure one-handed operation
Detachable shoulder strap for field workers
Built-in screen protector for scratch resistance
Multi functional tablet protective cases wholesale with these add-ons command 20-30% higher retail prices.
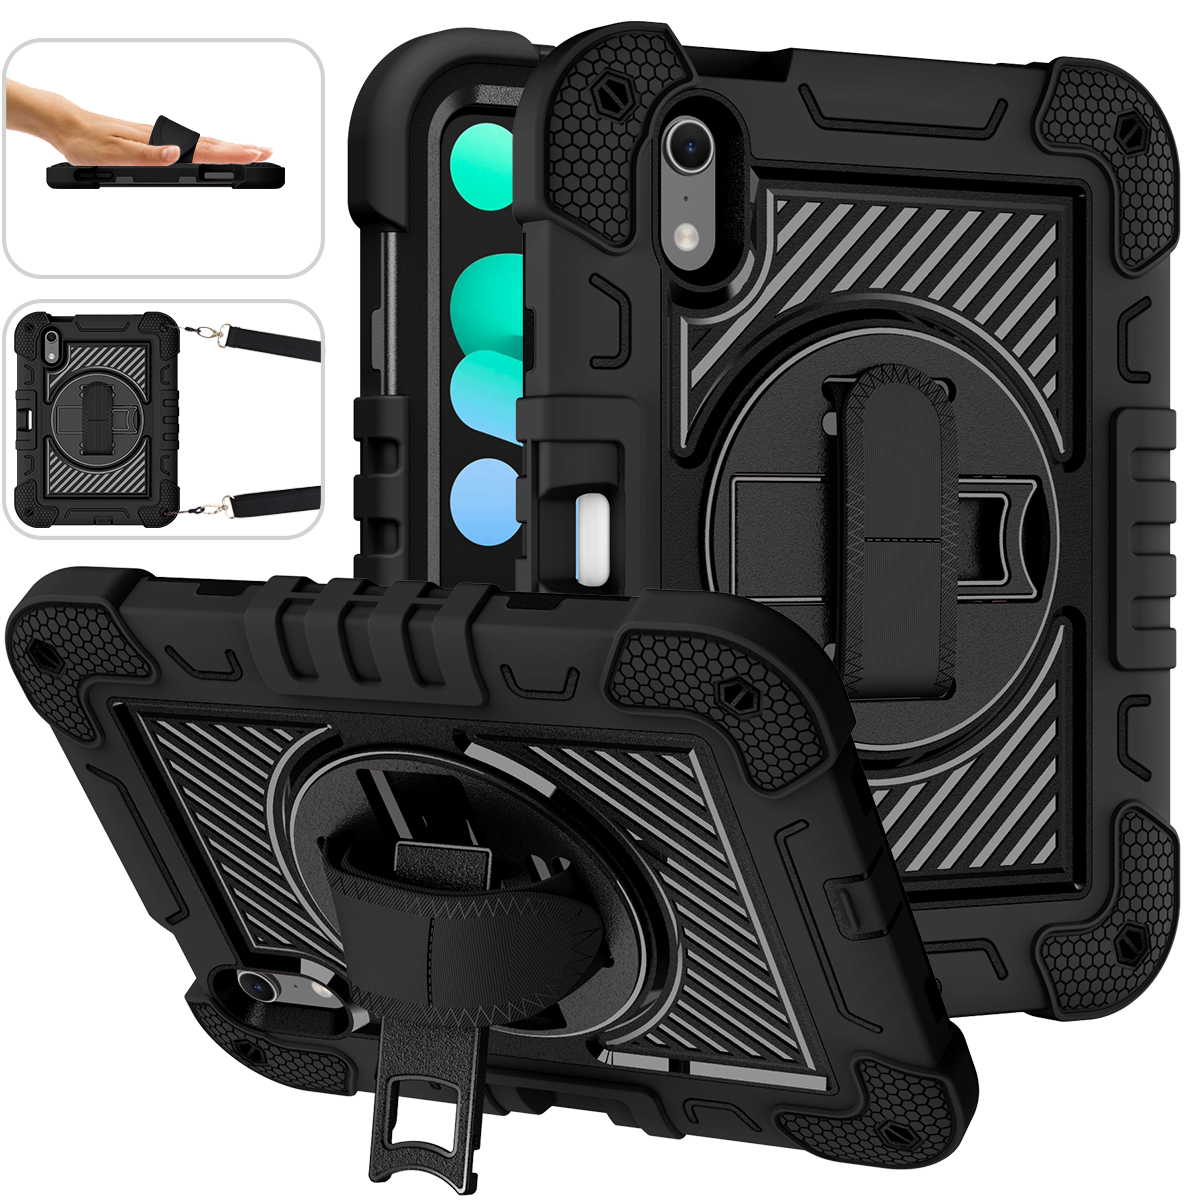
alt: tablet case with kickstand, hand strap, and shoulder strap features
4. Navigate Customization and Branding Options
Custom tablet cases for distributors help differentiate your brand and increase customer loyalty.
4.1 Customization Capabilities to Look For
A reliable tablet protective case wholesale supplier should offer:
Custom color matching (Pantone color system)
Logo printing (silk screen, UV printing, laser engraving)
Custom packaging design
Modified mold designs for unique features
Tablet case bulk order with multiple colors allows you to cater to different customer preferences without excessive inventory.
4.2 OEM/ODM Process Considerations
When working with a rugged tablet case manufacturer on custom projects:
Request a 3D render or prototype before mass production
Confirm tooling fees and production timelines
Schedule third-party quality inspections
Secure intellectual property protection agreements
For importers, partnering with an experienced tablet case supplier for importers ensures smooth customs clearance and compliance.
5. Calculate Total Cost and Ensure Supply Chain Reliability
The quoted unit price is only part of the total cost. Factor in all expenses to avoid budget overruns.
5.1 Total Cost of Ownership Breakdown
When evaluating wholesale iPad protective cases or other models, consider:
Unit product cost
Shipping and freight charges
Customs duties and taxes
Quality inspection fees
Potential return or warranty costs
5.2 Supply Chain Stability for 2026 and Beyond
Post-pandemic supply chain volatility continues in 2026. Ensure your supplier has:
Multiple raw material sources
Backup production facilities
Safety stock for popular models
Flexible order adjustment policies
For tablet cases for corporate device fleets or education deployments, supply chain reliability is non-negotiable to meet project deadlines.
In conclusion, selecting the right tablet case wholesale partner requires careful evaluation of product quality, supplier capabilities, customization options, and total cost. By following this guide, e-commerce sellers and B2B buyers can make informed decisions that drive business growth in 2026 and beyond.
Keywords:tablet case wholesale, tablet protective case wholesale supplier, rugged tablet case manufacturer, bulk tablet cases for business, wholesale iPad protective cases





+86 13422271740

info@tongmeitech.com

No. 34, Mashe Section, Guihe Road, Lishui Town, Foshan, Guangdong, China